Contact
Tel: 18037961302
Sales hot line ( 24 hours service): 18037961302
Sales hot line ( 24 hours service): 18037961302
E-Mail: firstfurnace@gmail.com
whatsapp:+8618037961302
Adress: Luoxin Industrial Park, Luoyang, HenanLarge AC Motors Terminal Rings
Medium-frequency welding of mo
Medium-Frequency Brazing Equip
Integral Brazing Process for t
Online Heating Equipment for T
Online Heating Equipment for A
Aluminum ingot heating equipme
Welding Equipment for Traction
Fully Digital Medium Frequency
Motor rotor end ring brazing e
Brazing equipment for hydro ge
Generator rod induction brazin
Hydropower generator stator ba
Large diameter steel pipe quen
Piston rod quenching and tempe
Grinding rod quenching and tem
Electric furnace technical information(技术)
1, regular
(1) On-site personnel shall wear labor protection articles in strict accordance with the company's requirements, and use special filters when observing high temperature metals.
(2) The furnace lining should be checked frequently at regular intervals to prevent “depletion”. Check the furnace lining after cooling: The thickness of the lining (excluding the asbestos board) must be repaired when the burning loss is less than 65mm~80mm. If there is no abnormality, forcefully remove it around 250 furnaces. The feeding should be carefully and carefully avoided to avoid the “cross-bridge” and “capping” of the material. The ultra-high temperature of the metal under the "bridge, cover" will cause the lining corrosion to accelerate.
(3) The charge should be dry, free of flammable materials, closed containers, and not excessive rust. The violent boiling of liquid or flammable materials in the charge can cause the molten metal to overflow or even explode.
(4) There shall be no water in the pit before the furnace to prevent the molten iron from splashing and exploding after pouring.
2. Intermediate frequency furnace feeding method
(1) Regardless of the charge, the next melt should be slowly injected before the previous charge is melted. If the rust and sand-filled charge are used incorrectly, the block size and shape are poor, the charge is not tightly packed and the stretch is severe, or if the cold charge is too much, the “bridge” is likely to occur. The liquid level must be checked frequently. Once the bridge occurs, it should be disposed of immediately, and the “bridge” should be removed to avoid the “bridge” formation. Otherwise, the lower iron will overheat, causing erosion of the lower lining, or even leakage of iron or explosion.
(2) Bridge treatment method: reduce the melting current to below 500A; use iron rod to smash and wear; if not treated, tilt the electric furnace properly, keep the low power melting until the molten iron breaks through the bridge or the capping layer;
(3) After the furnace material is completely melted, the slag should be slag immediately to prevent the formation of a "slag cover". If it is formed into a "slag cover", it should be immediately powered off, and the "slag cover" should be broken and thrown out of the furnace, otherwise the lower iron will overheat, causing erosion of the lower furnace lining, or even leakage of molten iron or explosion.
Large AC Motors Terminal Rings Medium-fr
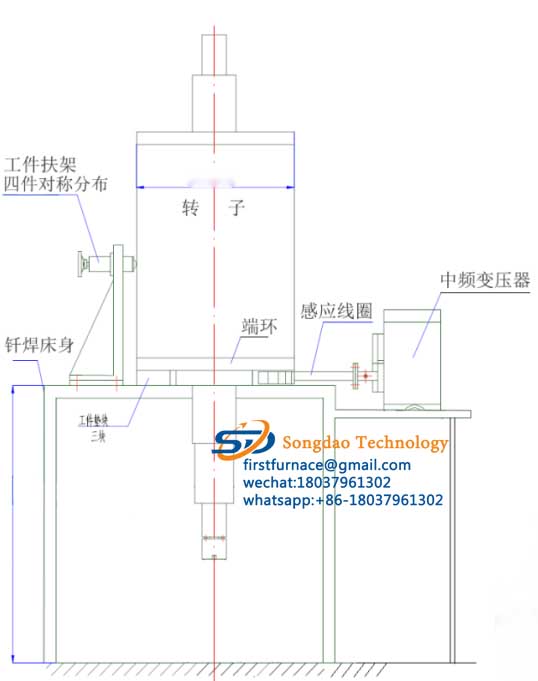
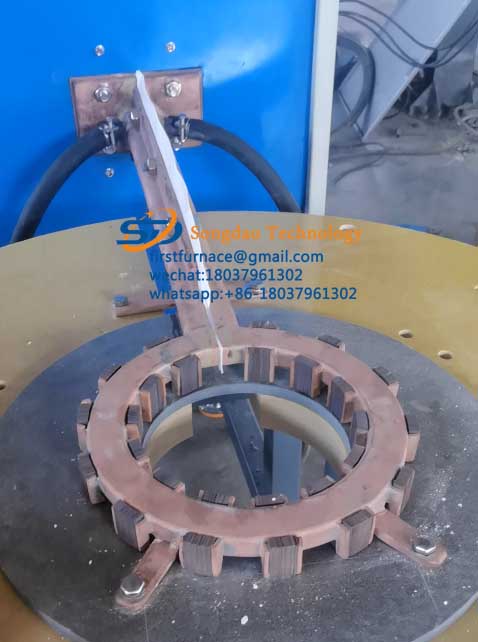
Electric Motor Rotor Bars and End Rings
Medium-frequency welding of motor rotors
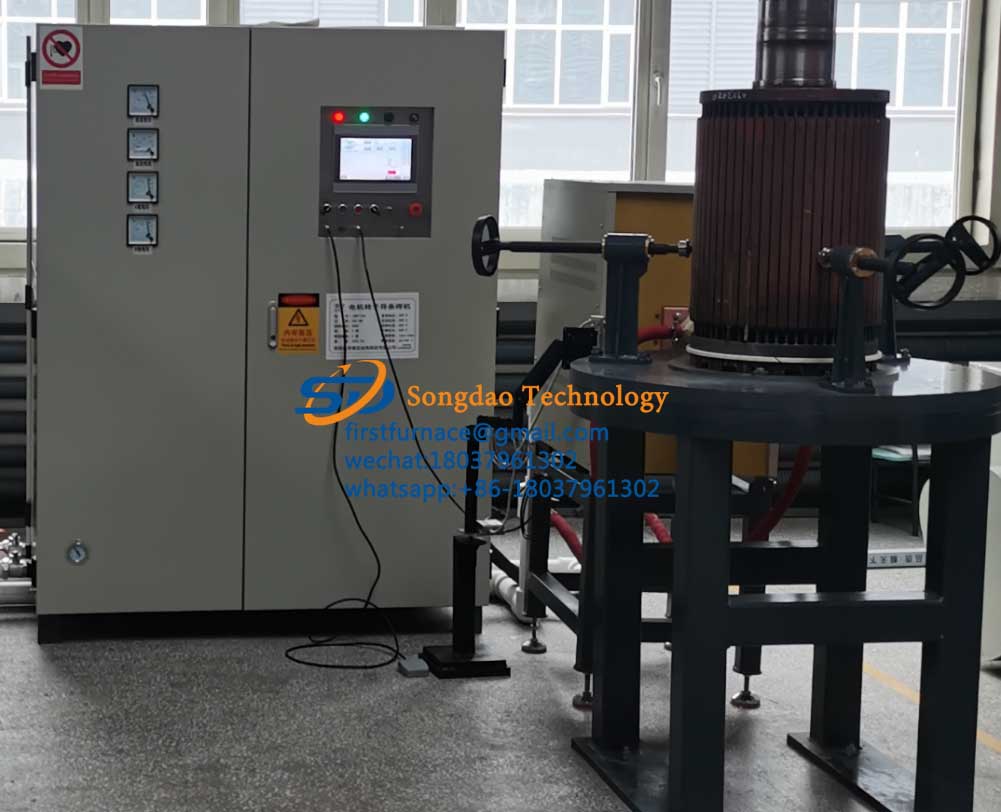
Medium-Frequency Brazing Equipment
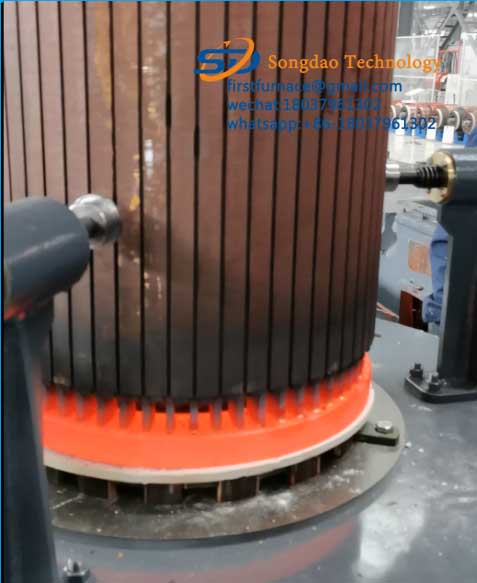
Integral Brazing Process for the Rotor E
Online Heating Equipment for Trapezoidal
Online Heating Equipment for Aluminum In
Aluminum ingot heating equipment
Welding Equipment for Traction Motor Rot
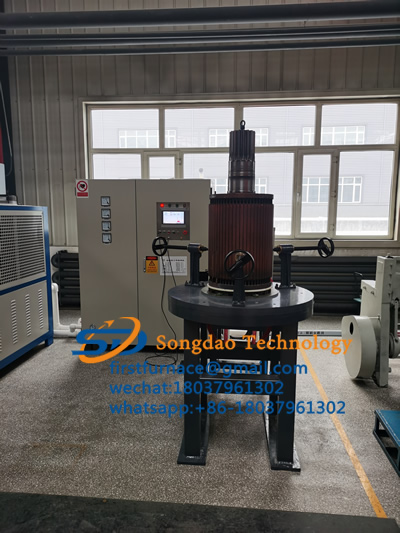
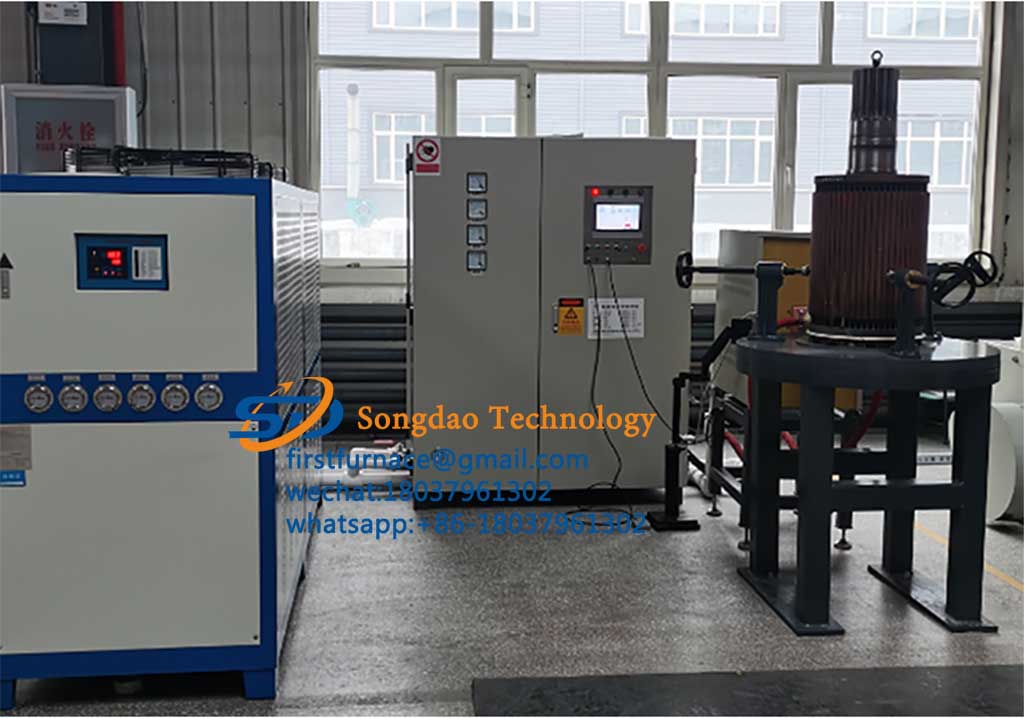
Fully Digital Medium Frequency Welding E
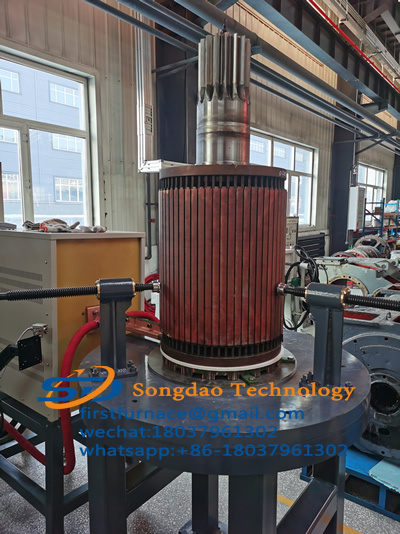
Motor rotor end ring brazing equipment
Motor Rotor Guide Bar Welding Heating Eq
Brazing equipment for hydro generator co
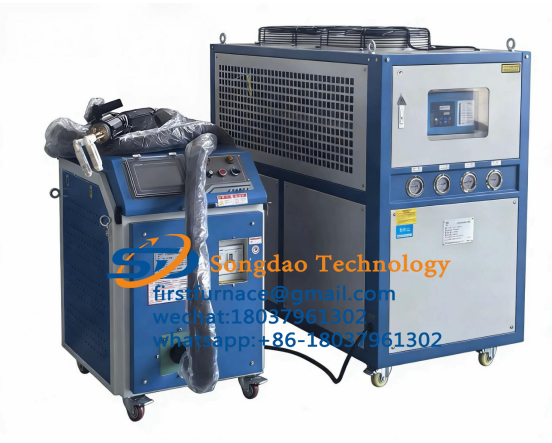
Generator rod induction brazing equipmen
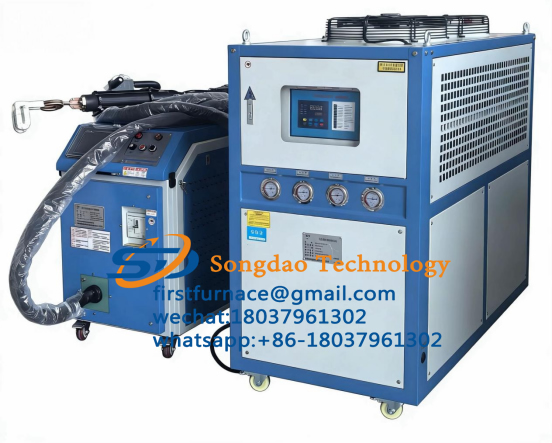
Hydropower generator stator bar brazing
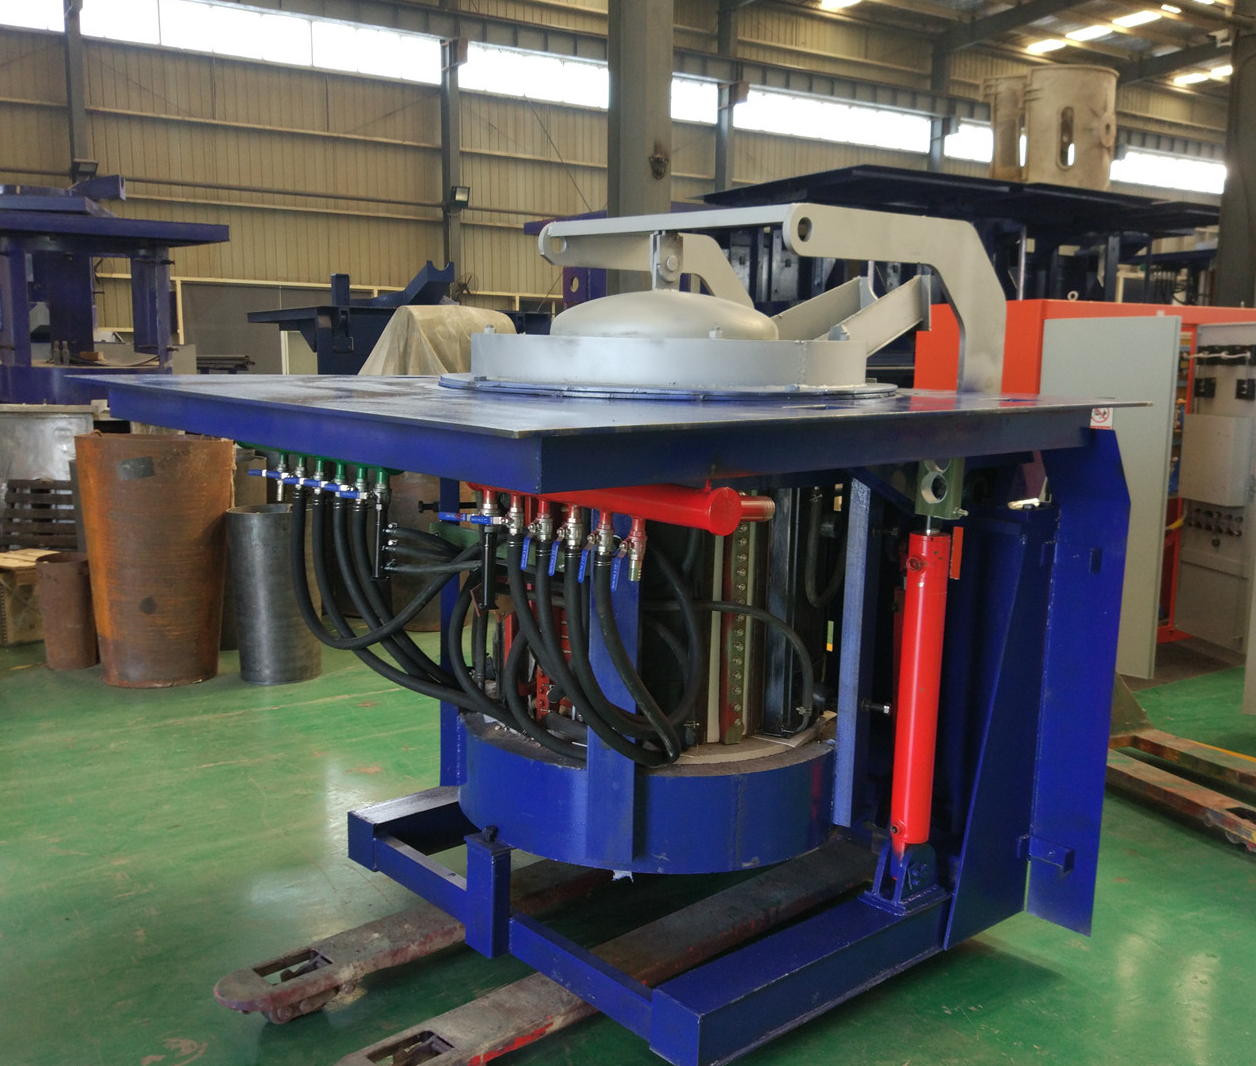
Iron induction furnace
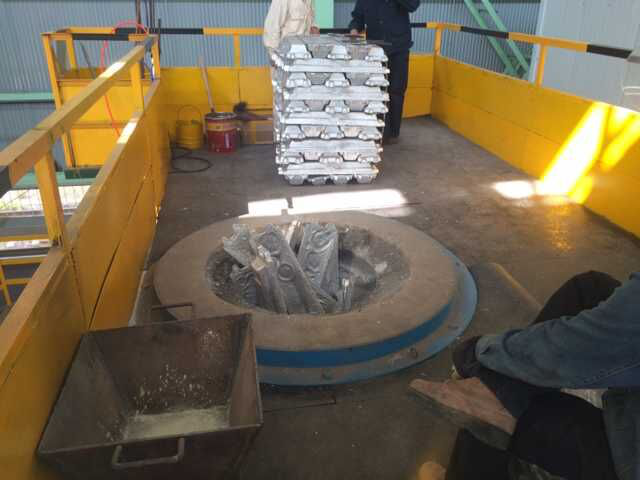
Aluminum melting furnace
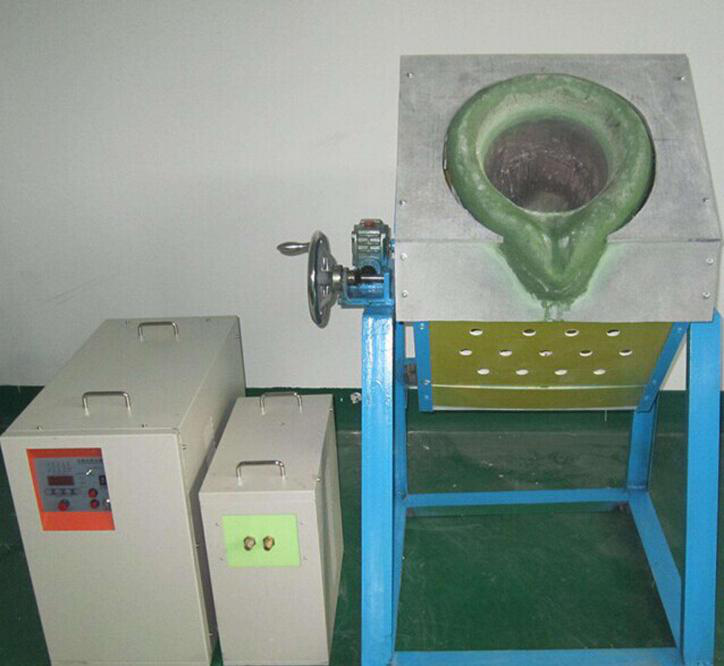
Copper melting furnace
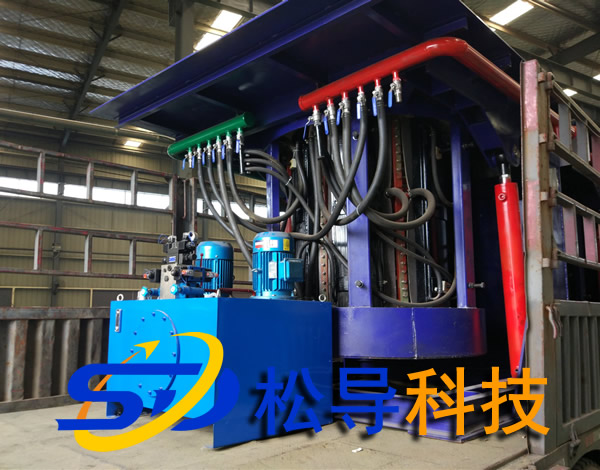
Small steel melting furnace
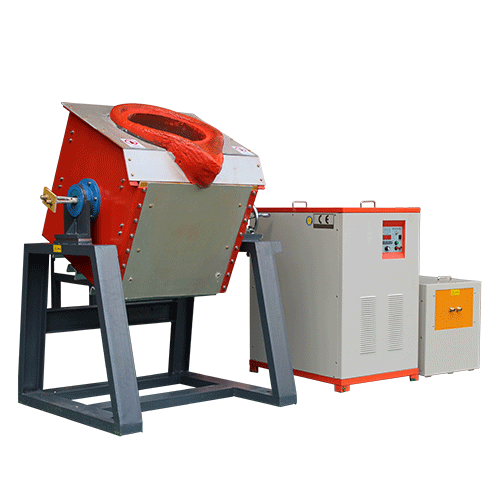
Small induction melting furnace
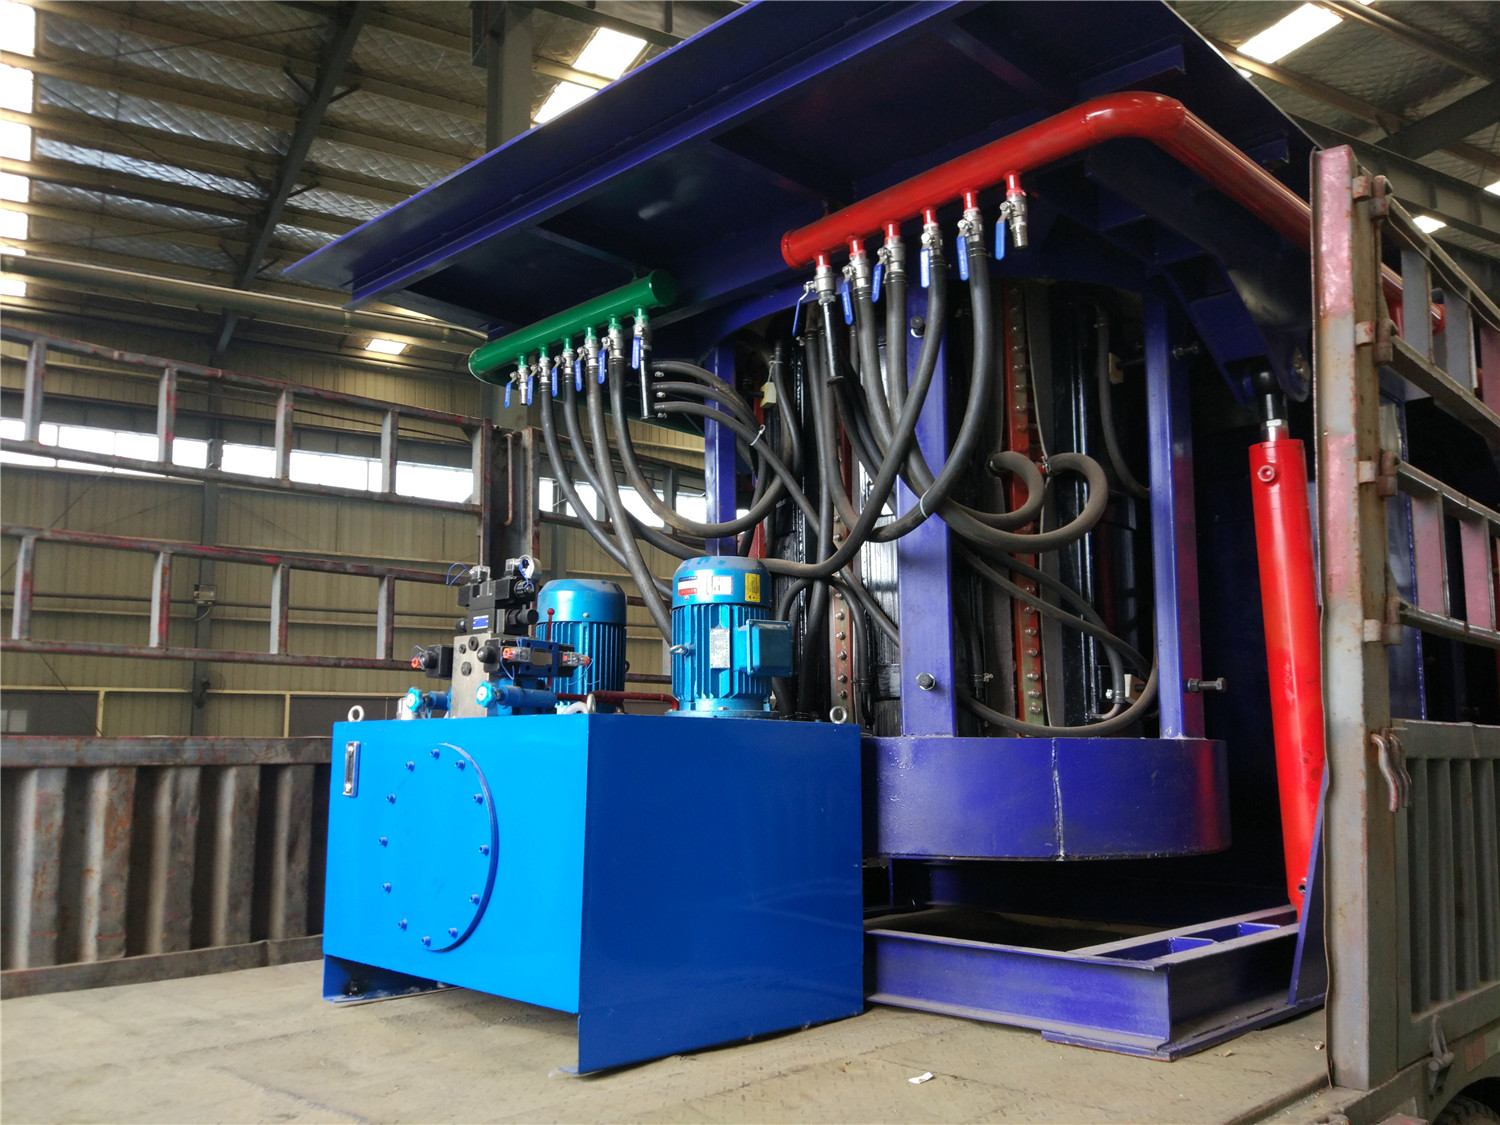
Induction iron furnace
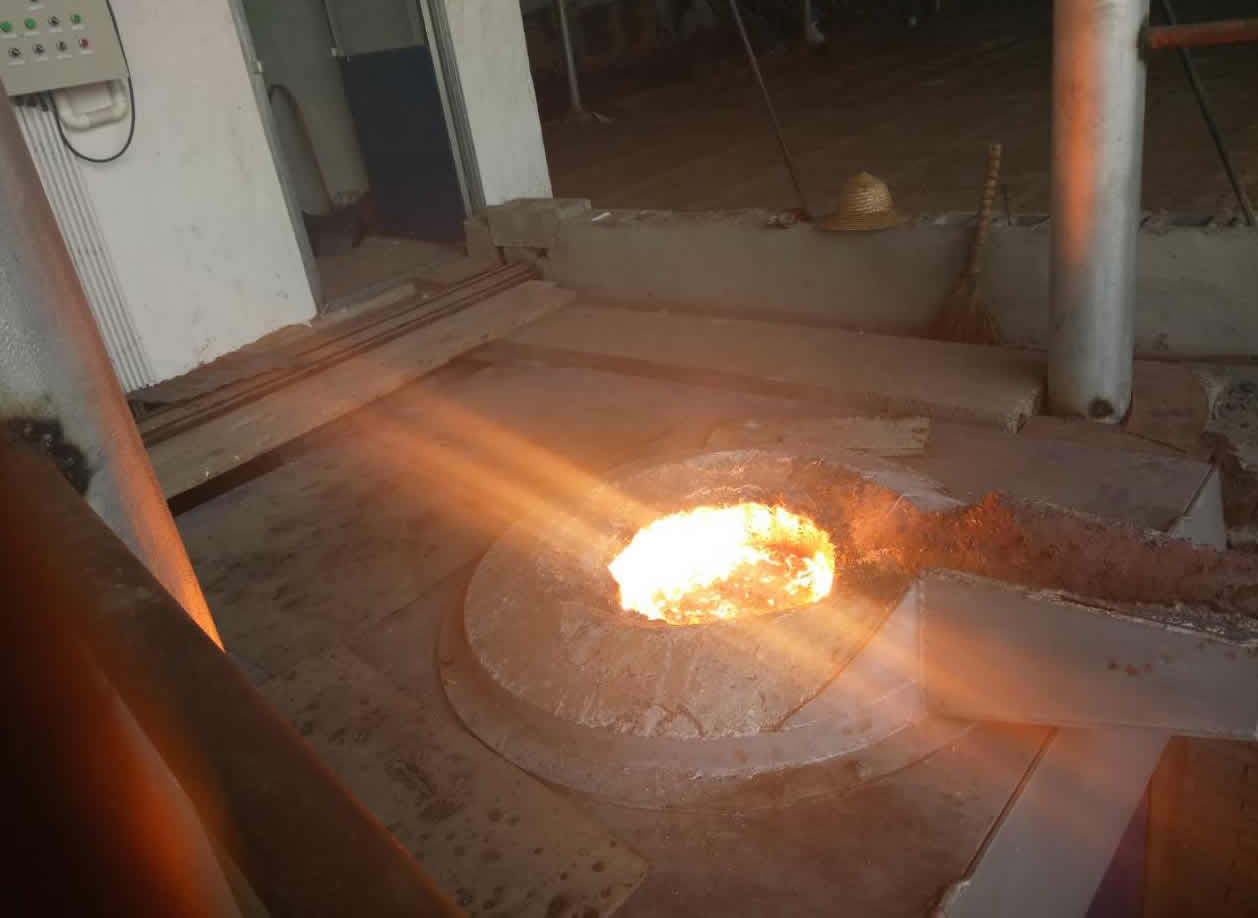
3T intermediate frequency iron melting f
0.25T Intermediate Frequency Furnace
0.5T Intermediate Frequency Furnace
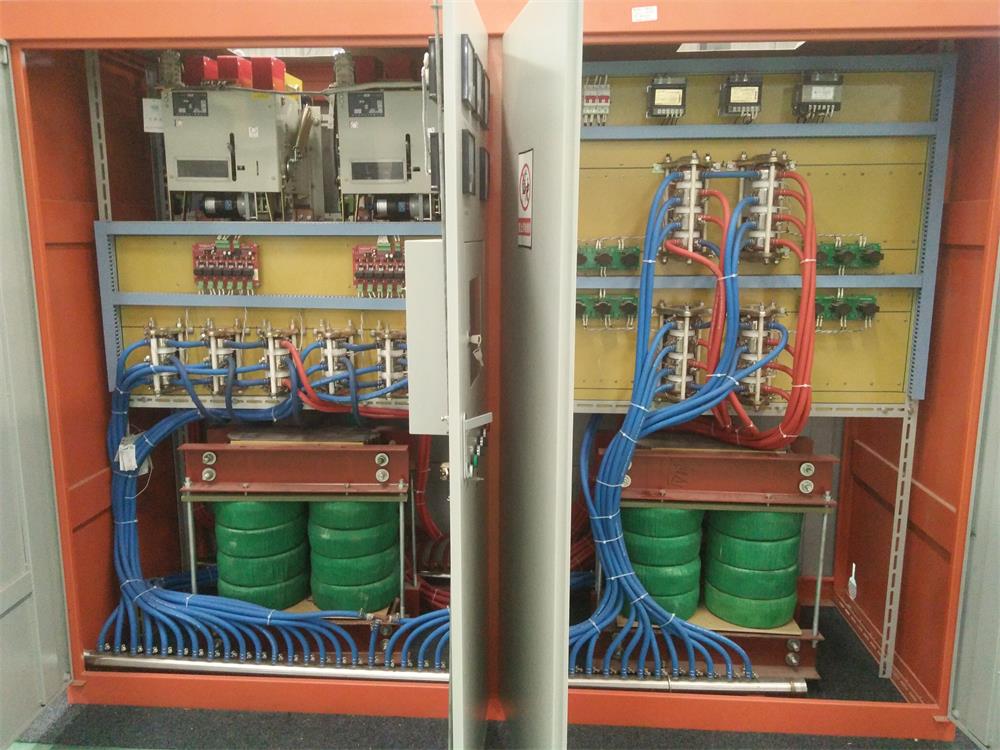
Medium Frequency Furnace

2T Induction Melting Furnace
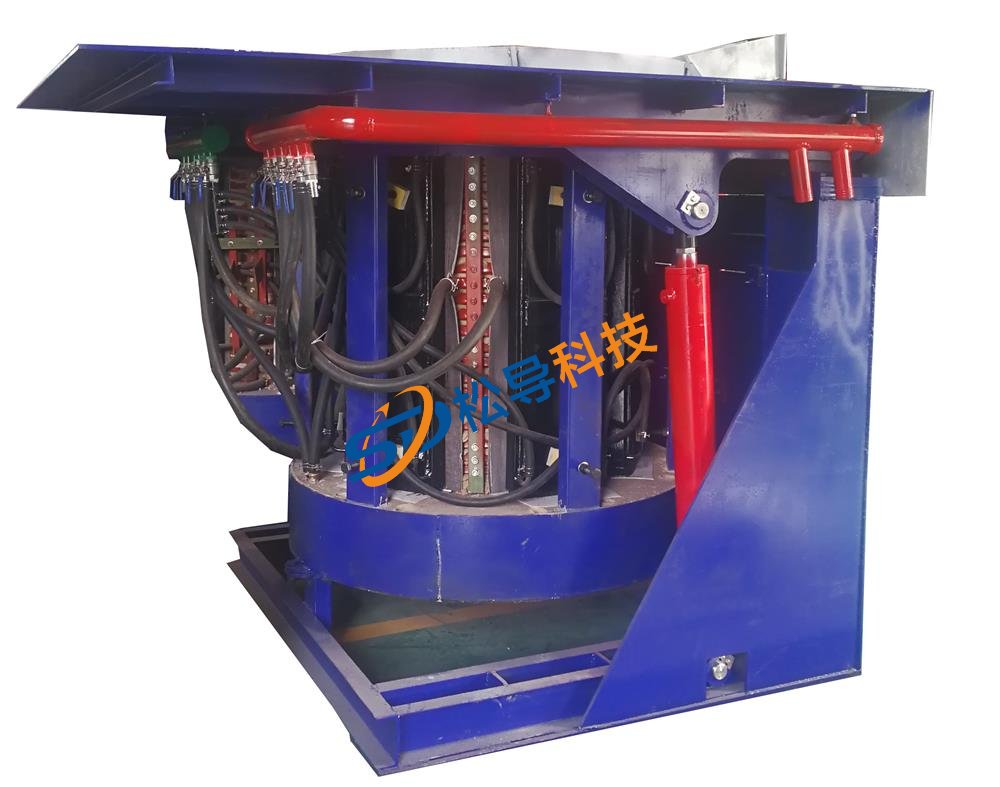
1T Induction Melting Furnace
500kg Induction Melting Furnace
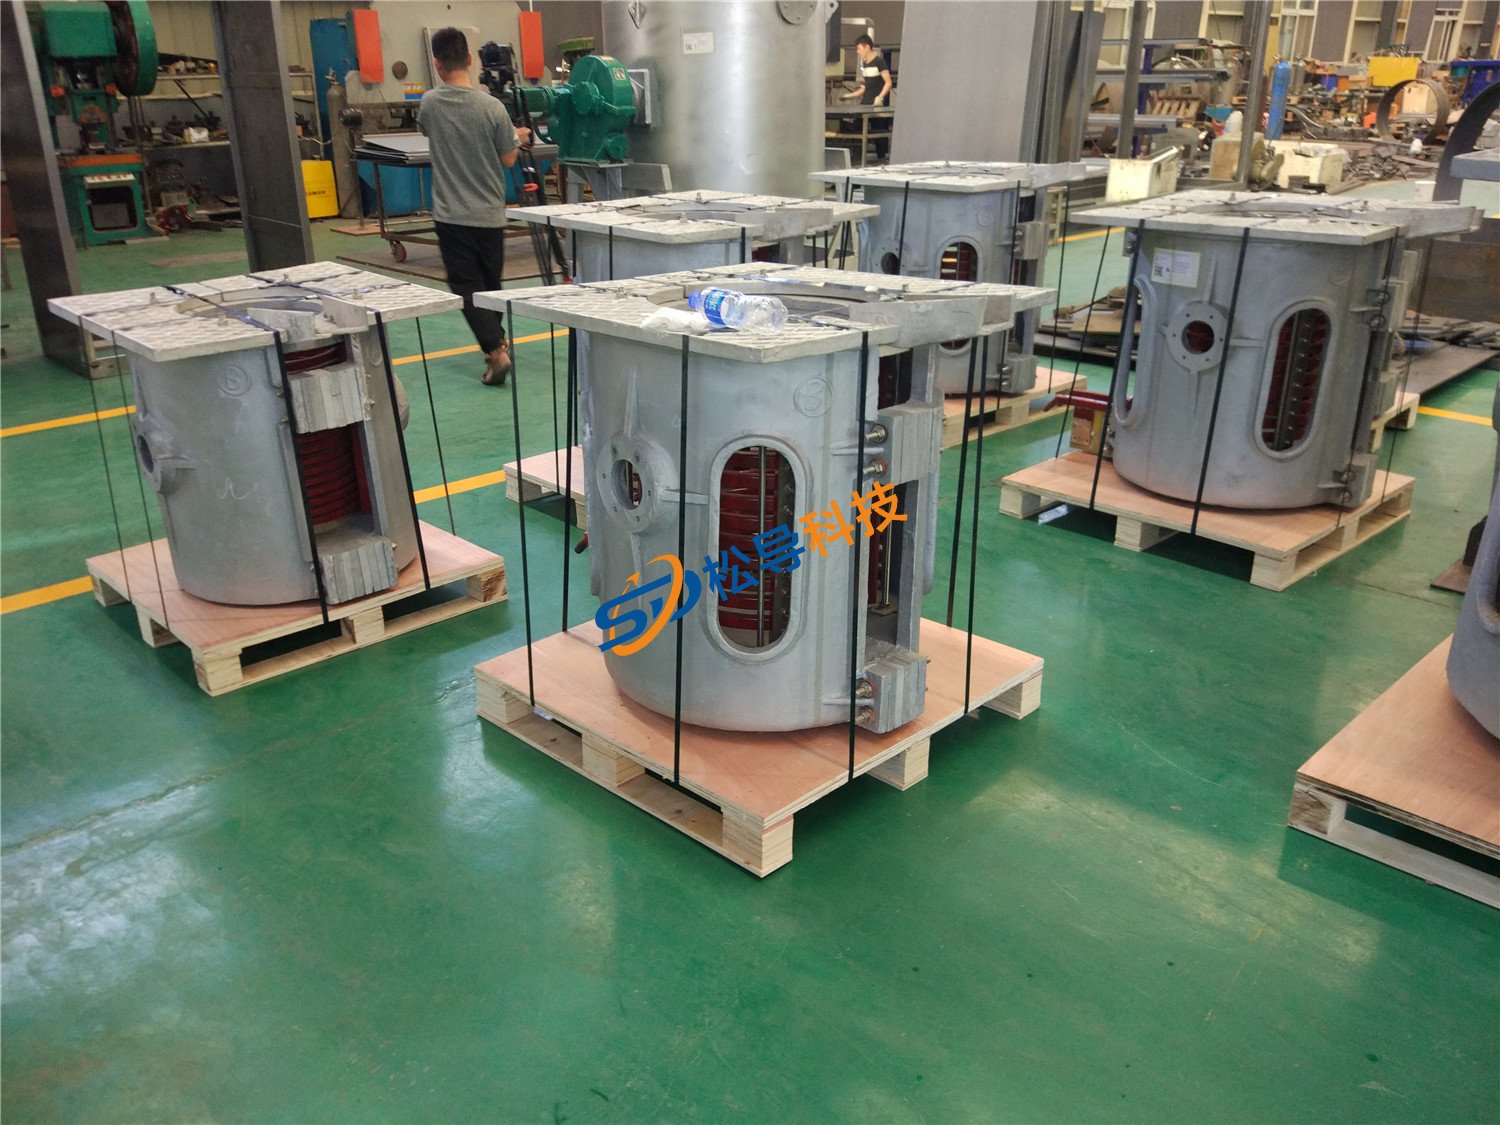
250kg Induction Melting Furnace
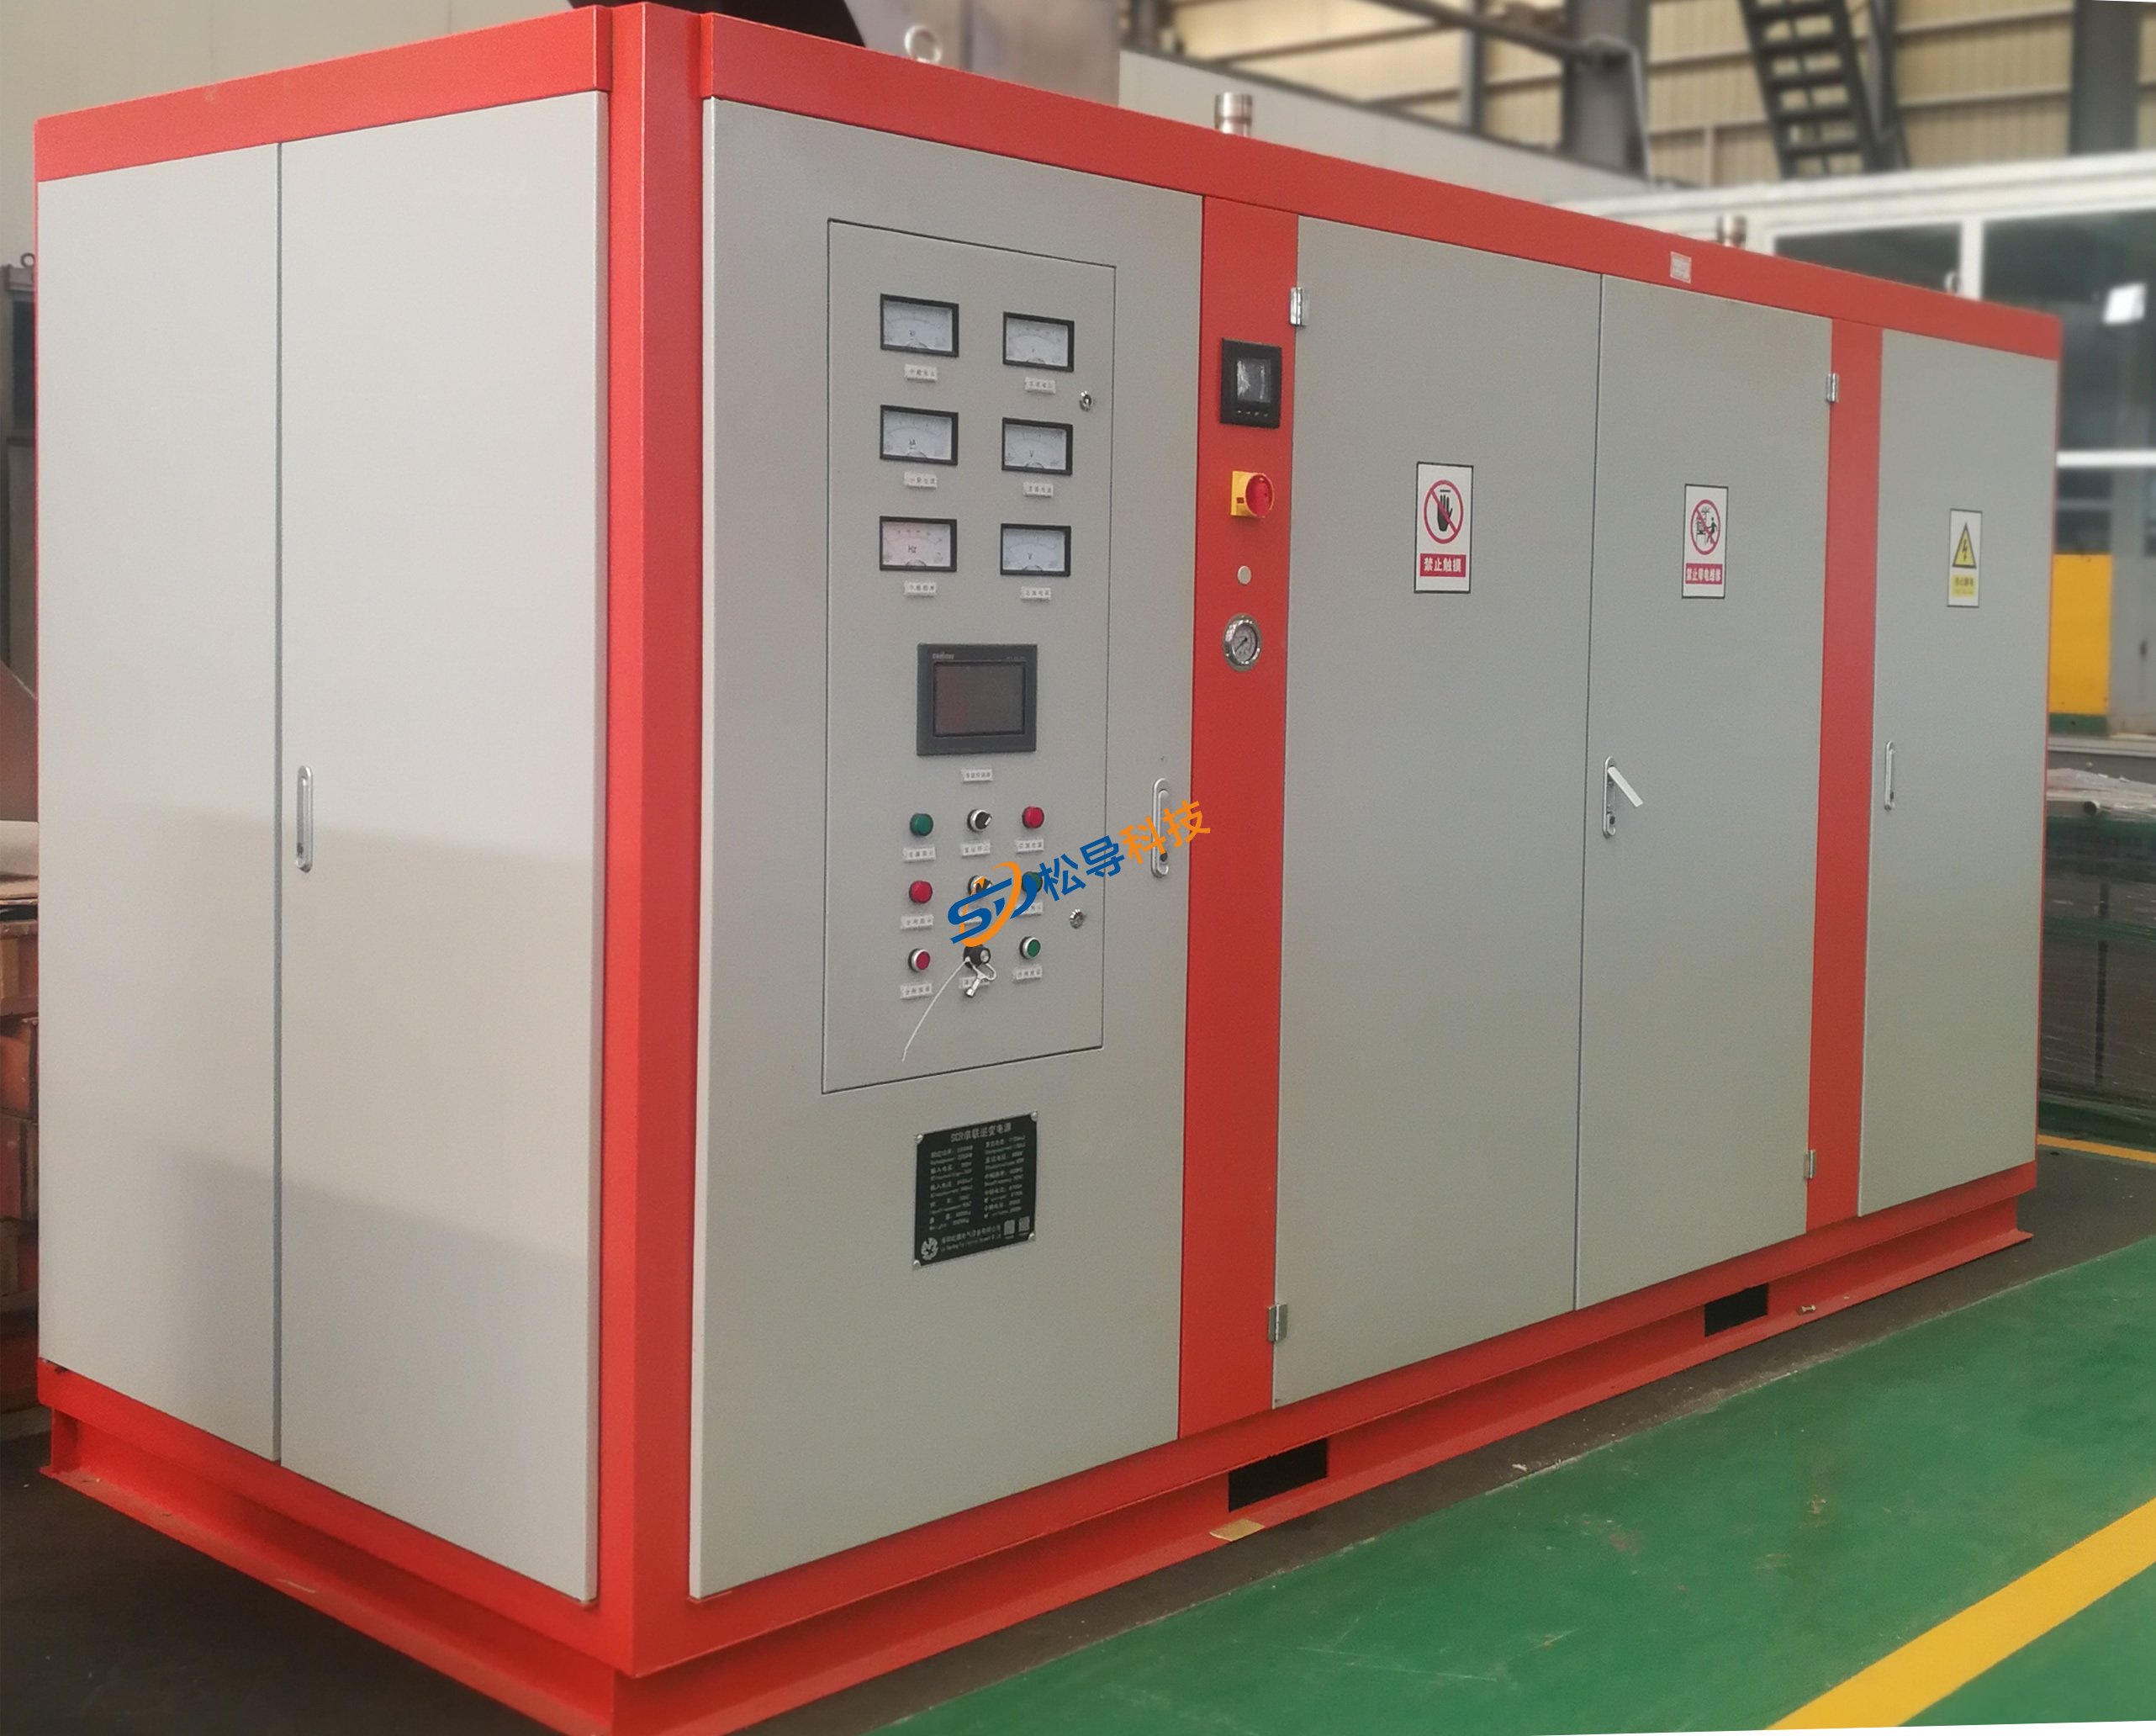
Induction Melting Furnace
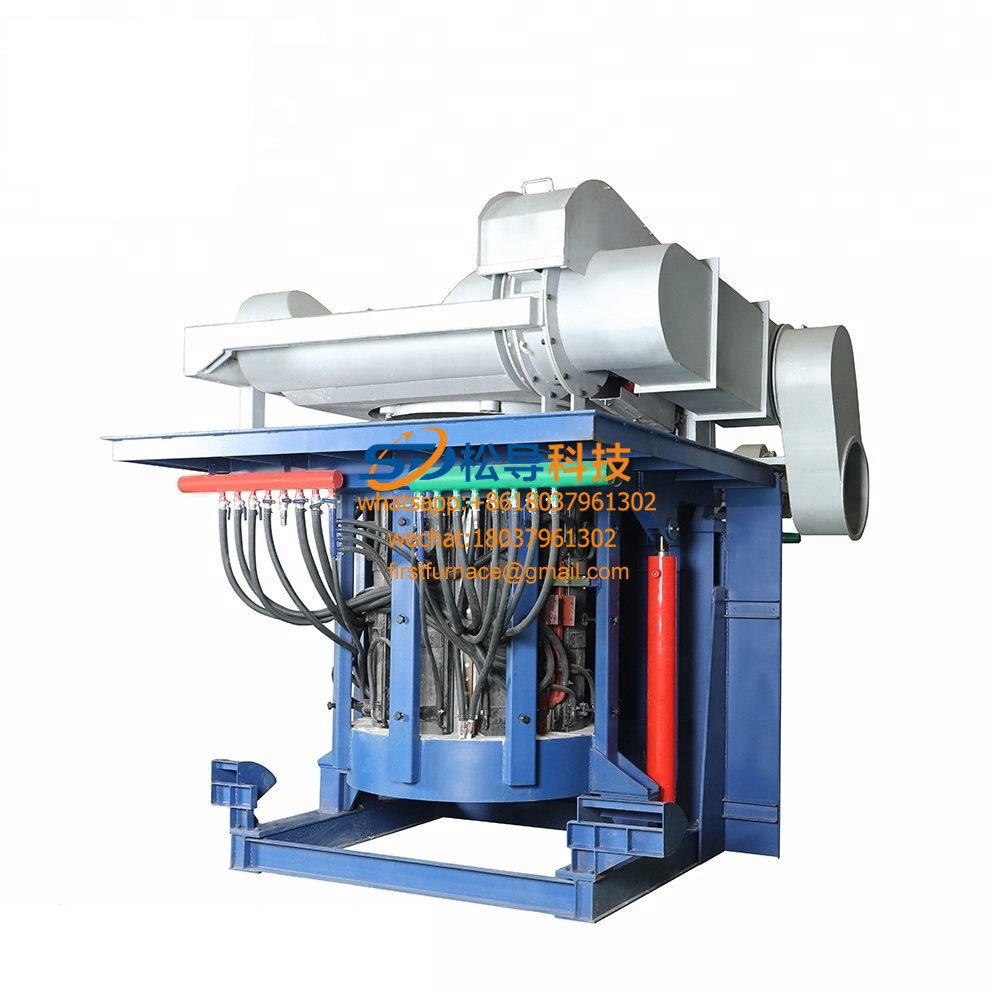
3 T Induction Melting Furnace
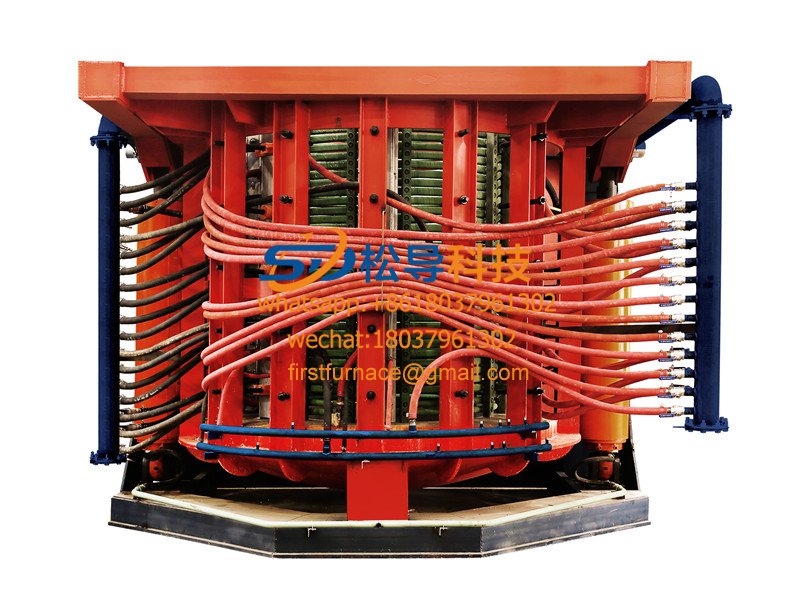
5T Induction Melting Furnace
Product Class